Top 7 Best Dehumidifier For Construction Site
The best dehumidifiers for construction sites are robust, high-capacity units like the ALORAIR 180 PPD Storm LGR and the Waykar 150 Pint Commercial, chosen for their durability, water damage restoration capabilities, and job site versatility.
Keeping construction environments dry is crucial for preventing mold growth, protecting materials, and ensuring a healthy work environment. These powerful machines are designed to handle the demanding conditions of active building projects, removing significant amounts of moisture to speed up drying times and maintain ideal humidity levels.
We’ve reviewed numerous models to bring you our top 7 picks for the best construction site dehumidifiers. Each unit was evaluated based on its moisture removal capacity, energy efficiency, portability, and overall value for money. Continue reading to explore our detailed comparison and find the perfect dehumidifier to keep your construction site dry and productive.
3 Standout Picks: Water Damage Restoration, Professional Drying, and Job Site Versatility
Start with these 3 standouts. Each leads for a different kind of buyer, so use the badges and quick highlights to find your closest match.


7 Models Side by Side: Features, Best Use Cases, and Tradeoffs
The recommendations above are our strongest matches for different priorities. Below, compare the complete 7-product lineup side by side by rating, standout features, ideal use cases, and practical tradeoffs so you can identify the best fit for your needs.
- 180 pint capacity
- Built-in pump
- 210 CFM airflow
- 180 pint capacity
- Built-in pump
- 210 CFM airflow
- 150 pint capacity
- Stackable design
- Built-in pump
- 155 pint capacity
- 7,500 sq ft coverage
- Built-in pump

- 150 pint capacity
- Panasonic compressor
- Built-in pump

- 125 pint capacity
- Compact design
- Energy-saving R32
- 113 pint capacity
- Compact, rugged design
- Auto-defrost system
7 Models Reviewed in Depth
#1. ALORAIR 180 PPD Storm LGR
Max Capacity
Airflow
Pump Drainage
When water damage strikes, the ALORAIR Storm LGR Extreme is engineered to perform, boasting an exceptional 180-pint capacity and a powerful 210 CFM airflow to rapidly dry out large spaces up to 2,300 sq. ft. Its integrated pump and extended drain hose offer flexible drainage solutions, crucial for continuous operation during restoration jobs. Features like auto-restart and auto-defrost minimize downtime and ensure reliable performance when you need it most.
Despite its robust capabilities, the 64.3 lb weight means it’s best suited for professional use where portability is managed by a team or dedicated transport. If your priority is maximum moisture removal speed and reliability for critical restoration projects, this ALORAIR unit is a top-tier investment, further solidified by its comprehensive 6-year warranty.
Pros
- Extremely high moisture removal rate
- Powerful airflow for rapid drying
- Reliable with auto-features
Cons
- Heavy and bulky
- Higher price point
- Primarily for professional use
Specifications
#2. ALORAIR 180 PPD Storm LGR
Max Capacity
Airflow
Pump Drainage
The ALORAIR Storm LGR Extreme in green is a high-performance dehumidifier designed for the rigors of professional drying and water damage restoration. It boasts an impressive 180-pint capacity and a substantial 210 CFM airflow, capable of tackling large areas up to 2,300 sq. ft. quickly and efficiently. The integrated pump and generous drain hose length simplify continuous operation, a critical factor on demanding job sites where uninterrupted drying is paramount.
While its 64.3 lb weight signifies a robust build, it requires careful handling for transport. The unit includes auto-defrost and auto-restart features, ensuring reliable performance even in challenging conditions. For professionals prioritizing speed, capacity, and reliability in water damage scenarios, this ALORAIR model is an excellent, albeit heavy, choice.
Pros
- Exceptional drying capacity
- High airflow for speed
- Built-in pump simplifies drainage
Cons
- Heavy and bulky unit
- Best suited for professionals
- Requires consistent power source
Specifications
#3. Waykar 150 Pint Commercial
Daily Capacity
Design
Pump Drainage
The Waykar 150 Pint Commercial Dehumidifier is a standout for its blend of power and practical design, perfect for construction sites and versatile job site use. It delivers an impressive 150-pint capacity across a vast 7,500 sq. ft. area, ensuring rapid drying. The built-in pump and included 16-ft hose simplify drainage, while the unique stackable design is a game-changer for professionals needing to maximize storage space.
While it offers excellent portability features like wheels and multiple handles, its 56.3 lb weight still requires some effort to move. The dual dehumidification modes (Auto and Continuous) add flexibility, and features like auto-defrost and memory restart enhance reliability. This Waykar unit is a smart investment for professionals who value performance, space-saving storage, and convenient operation.
Pros
- High capacity and coverage
- Stackable for storage efficiency
- Built-in pump and flexible drainage
Cons
- Moderately heavy
- Warranty requires registration
- Stacking requires care
Specifications
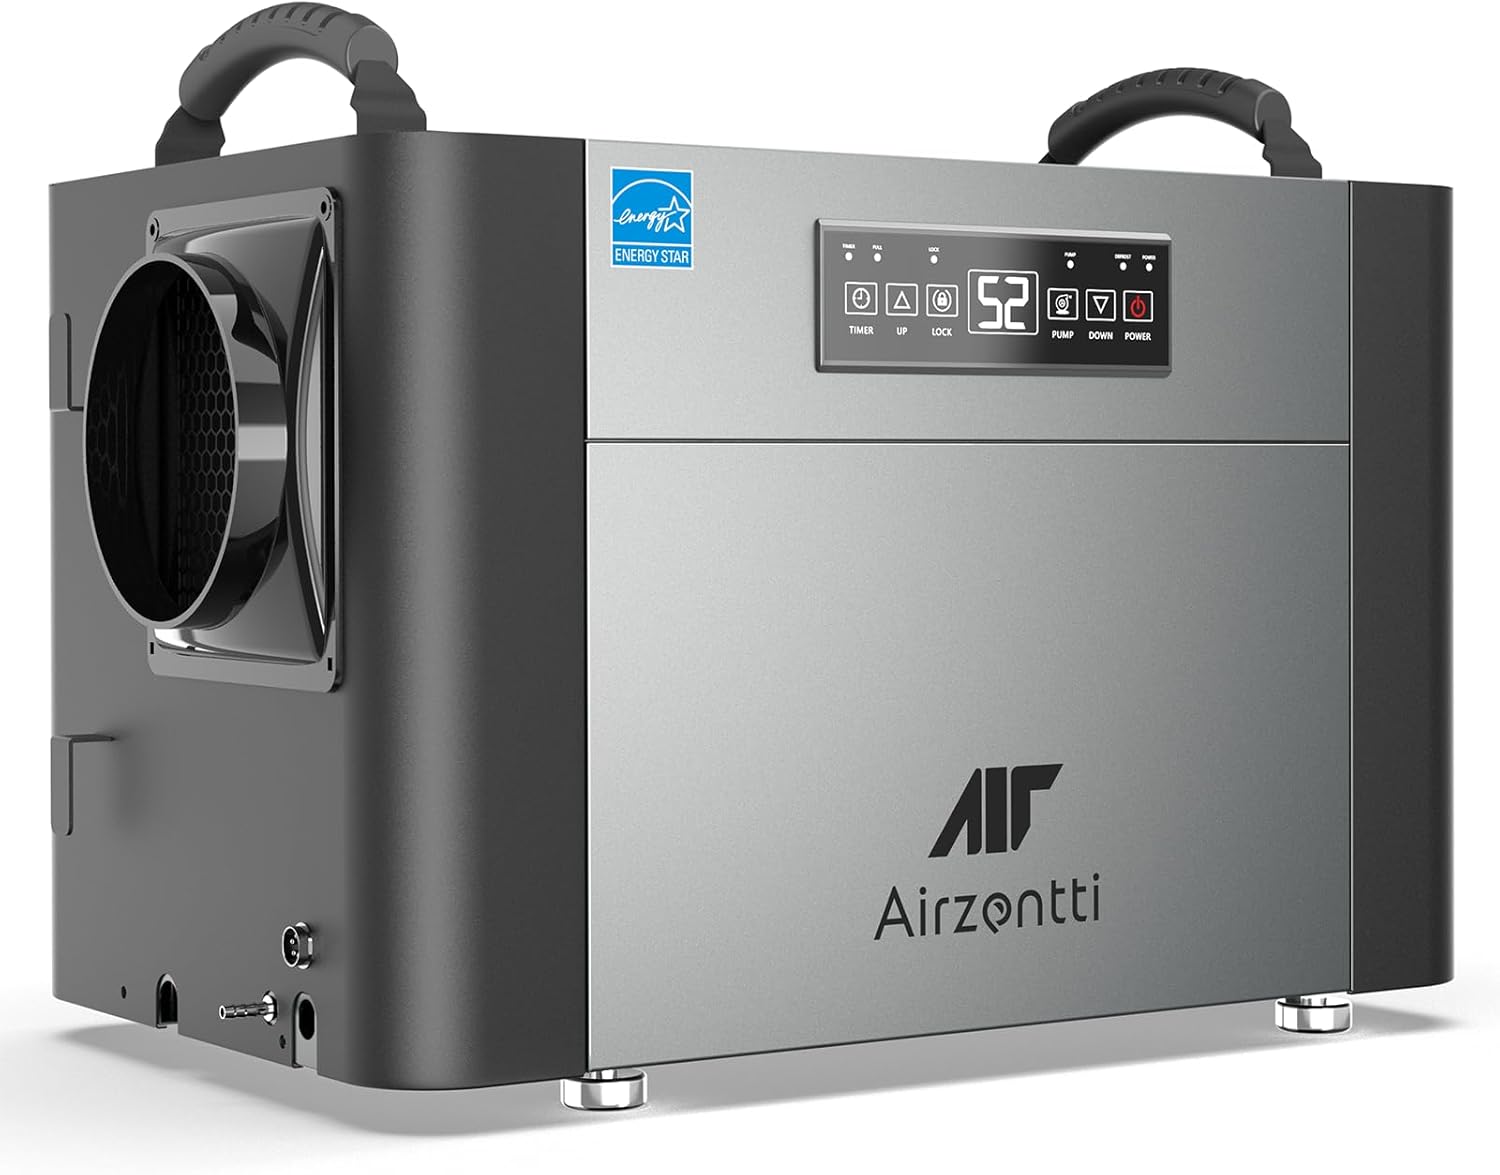
#4. Airzentti 155 Pint Commercial
Daily Capacity
Coverage Area
Pump Drainage
This Airzentti commercial dehumidifier is a powerhouse for construction sites and large spaces, boasting an impressive 155-pint capacity that can handle up to 7,500 square feet. Its built-in pump and auto-drain features simplify operation, allowing for continuous use without constant monitoring. The unit is also Energy Star certified, indicating good energy efficiency for its robust performance.
While its capacity and coverage are excellent for demanding environments, be aware that its weight of 60 lbs might make frequent repositioning a bit of a workout. It’s an ideal choice if you need serious moisture removal for extended periods on a job site or in a large commercial area, but perhaps less suited for frequent, quick moves between smaller locations.
Pros
- High capacity for large areas
- Built-in pump for continuous drainage
- Energy Star certified
Cons
- Heavy at 60 lbs
- Requires dedicated space
- Higher initial cost
Specifications
#5. MOUNTO 150 Pint LGR
Daily Capacity
Compressor
Pump Drainage
The MOUNTO 150 Pint LGR Dehumidifier is a robust option for serious water damage restoration and construction needs, featuring a high 150-pint capacity and a powerful Panasonic compressor for efficient moisture removal. Its 350 CFM airflow ensures quick drying across spaces up to 2,500 sq. ft. The integrated pump simplifies drainage, and the memory restart function is invaluable for maintaining continuous operation during power interruptions common on job sites.
While its 65 lb weight indicates solid build quality, it demands careful handling during transport. The copper tubing is a nice touch for durability. If you prioritize a high-capacity unit with a reliable compressor and built-in pump for demanding restoration tasks, this MOUNTO model offers excellent performance and value.
Pros
- High capacity and airflow
- Reliable Panasonic compressor
- Built-in pump included
Cons
- Heavy unit at 65 lbs
- Coverage area smaller than some
- No explicit auto-defrost mentioned
Specifications
#6. Airecoler 125 Pint Commercial
Design
Max Capacity
Refrigerant
The Airecoler GT-X5 is an excellent choice for construction sites and tight spaces, offering a substantial 125-pint capacity in a remarkably compact form factor. Its dimensions make it ideal for fitting into low-clearance crawl spaces or cramped basements, while still covering up to 6,000 sq. ft. The use of R32 refrigerant contributes to its energy-saving efficiency, and features like auto-defrost and auto-restart add to its convenience.
While it includes a drain hose, the built-in pump is an optional add-on, which might be a consideration for sites requiring vertical drainage. If you need powerful dehumidification that can squeeze into tight spots and offers energy efficiency, this Airecoler unit is a top-tier option, backed by a solid 5-year warranty.
Pros
- Very compact for tight spaces
- High capacity for its size
- Energy-efficient R32 refrigerant
Cons
- Pump is optional, not standard
- Slightly lower airflow than some
- Warranty details could be clearer
Specifications
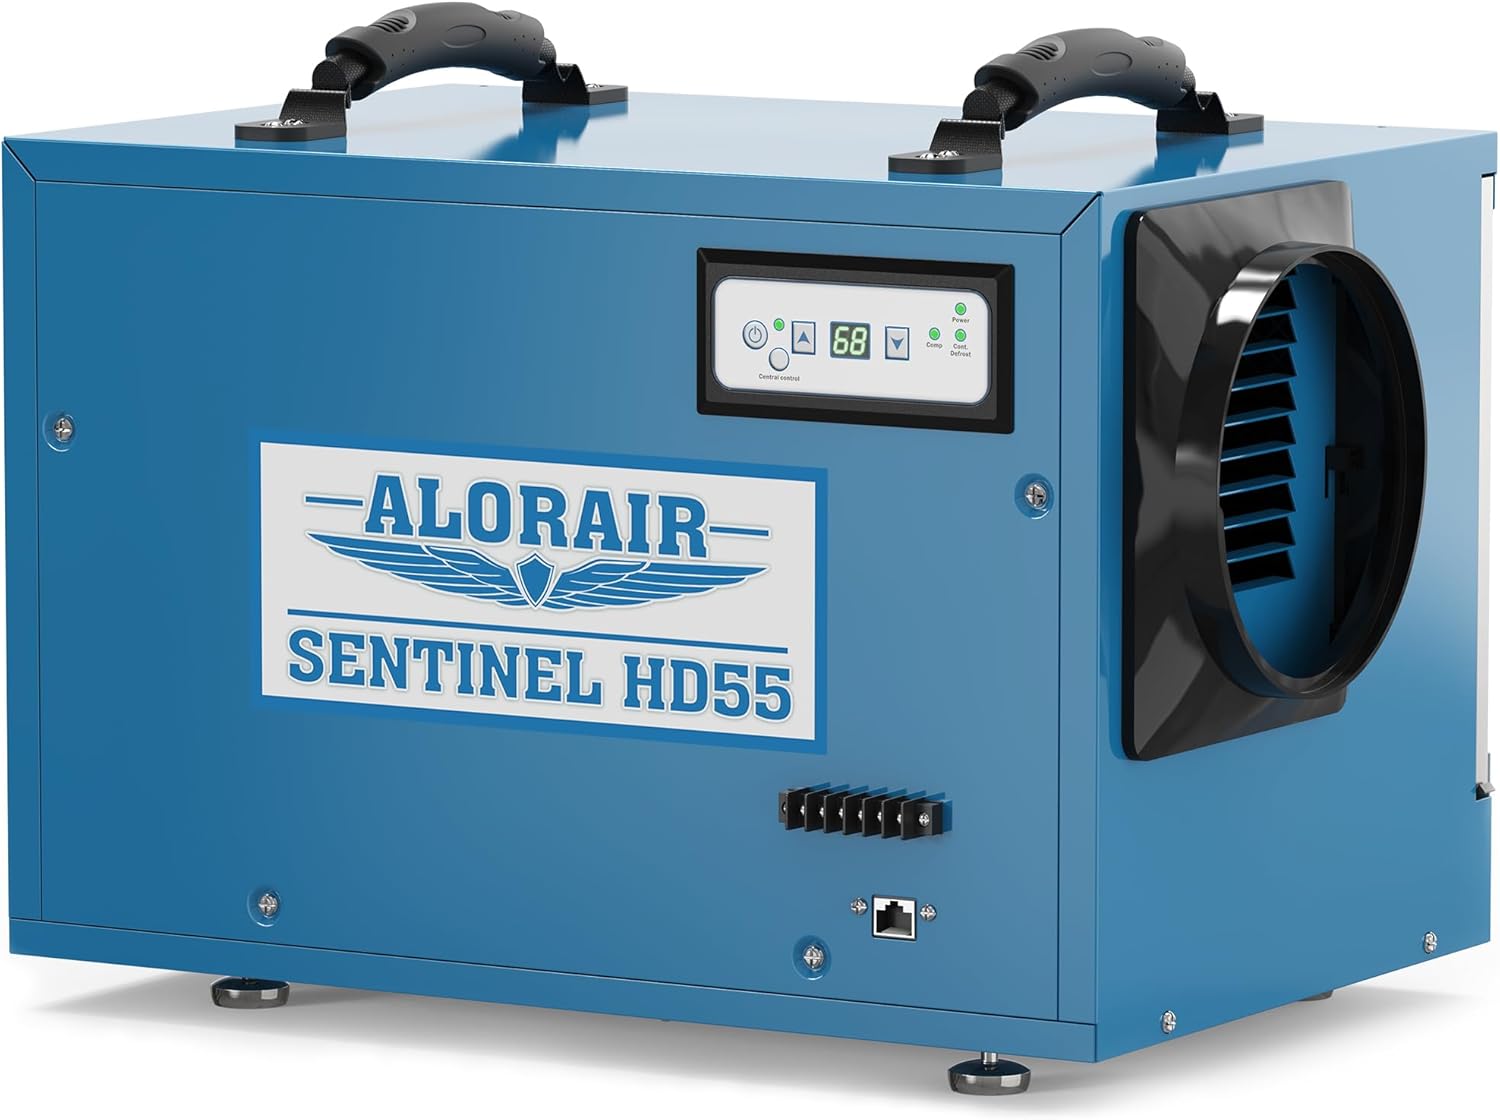
#7. ALORAIR Sentinel HD55
Daily Capacity
Metal Casing
Limited Warranty
The ALORAIR Sentinel HD55 is a solid choice for tackling humidity in basements and crawl spaces, offering a 113-pint capacity suitable for areas up to 1,200 sq. ft. Its compact and rugged metal casing is built to withstand tougher conditions, making it a reliable workhorse for job sites. The automatic defrost system ensures continuous operation even in cooler temperatures, and the auto-drain feature means you won’t be emptying tanks constantly.
While it’s designed for portability, its 41.7 lb weight means it’s not feather-light for constant relocation. If you need a durable, set-and-forget solution for persistent dampness in smaller commercial spaces or residential basements, this unit is a strong contender, especially with its impressive 6-year warranty.
Pros
- Durable metal construction
- Automatic defrost and drainage
- Long 6-year warranty
Cons
- Moderate weight for portability
- Lower coverage area than some
- No built-in pump
Specifications
Taming the Damp: Your Construction Site Dehumidifier Deep Dive
Construction sites are dynamic environments, and while progress is the goal, excess moisture can be a silent saboteur. From protecting materials to ensuring a healthy workspace, a robust dehumidifier isn’t just a convenience; it’s a crucial tool. Investing wisely means selecting a unit built for the rigors of the job, so let’s break down what truly matters.
The Non-Negotiables for Site-Ready Moisture Control
When you’re evaluating dehumidifiers for a construction setting, several key characteristics will dictate performance and longevity. Don’t get bogged down in jargon; focus on these practical elements.
- Robust Build Quality: Construction sites are tough. Look for units with durable casings, sturdy handles, and components designed to withstand dust, dirt, and occasional bumps. A metal housing often signifies greater resilience than plastic.
- Serious Moisture Removal Capacity: Consider the square footage you need to cover and the typical humidity levels you encounter. Higher cfm (cubic feet per minute) ratings generally mean faster drying and better air circulation, essential for large or particularly damp areas.
- Efficient Operation in Varied Temperatures: Construction projects can span seasons. Ensure the dehumidifier is designed to operate effectively across a range of temperatures, as performance can degrade in colder conditions.
- Drainage Options: Continuous operation is key. A unit with a built-in pump or a gravity drain hose connection will prevent frequent emptying, allowing the machine to work uninterrupted for longer periods.
- Portability and Placement: While not always the lightest, a good site dehumidifier should be manageable to move between areas. Consider the location of power outlets and how easily the unit can be positioned for optimal airflow.
Common Pitfalls That Can Dampen Your Project
Navigating the world of dehumidifiers can sometimes lead you astray if you’re not careful. Avoid these common missteps to ensure your investment pays off.
- Overlooking the power cord length and durability. A flimsy cord on a construction site is a hazard and an inconvenience.
- Choosing a unit that’s undersized for the space, leading to inefficient drying and wasted energy.
- Ignoring the noise level; while a construction site is rarely quiet, an excessively loud unit can impact worker comfort and communication.
Your Construction Site’s Moisture-Fighting Champion
When it comes to taming humidity on the job, the ALORAIR 180 PPD is your heavy-hitter for extreme moisture issues, while the Waykar 150 Pints is a powerhouse for large spaces needing consistent dryness. For those prioritizing energy efficiency and robust performance, the 155 Pint Commercial Dehumidifier is a solid choice. The MOUNTO 150 Pint LGR offers excellent LGR technology for tough jobs, and the 125 Pints Commercial Dehumidifier is ideal for smaller, persistent dampness. Finally, the ALORAIR Sentinel HD55 is your go-to for dedicated crawl space control.
All these units are built to tackle the demanding environment of a construction site, ensuring your projects stay on track and free from moisture-related setbacks. Don’t let dampness win – click the buttons above to check current availability and secure your chosen moisture solution today!
Final 3 Picks: Water Damage Restoration, Professional Drying, and Job Site Versatility
Ready to decide? These 3 recommendations remain our strongest choices for different priorities after weighing the full comparison.
