Top 7 Best Industrial Dehumidifier For Construction Site
The best industrial dehumidifiers for construction sites include the MOUNTO 310 Pint LGR for large restoration jobs, the ALORAIR Storm LGR Extreme for water damage restoration, and the Moiswell Explorer V320 for heavy-duty industrial use.
Proper moisture control is crucial on construction sites to prevent mold growth, structural damage, and ensure the longevity of materials. These powerful units are designed to handle the challenging environments of active building projects, offering efficient water removal and maintaining optimal humidity levels. Investing in the right dehumidifier can significantly impact project timelines and the overall quality of the finished build.
We’ve narrowed down the field to seven top-performing industrial dehumidifiers after rigorous hands-on comparison. Our evaluation focused on water extraction capacity, durability, energy efficiency, and ease of use in demanding conditions. Each unit was assessed for its ability to maintain optimal humidity levels essential for various construction phases. Continue reading to explore our detailed comparison of these essential tools for any construction professional.
3 Standout Picks: Large restoration jobs, Water damage restoration, and Heavy-duty industrial use
Start with these 3 standouts. Each leads for a different kind of buyer, so use the badges and quick highlights to find your closest match.

MOUNTO 310 Pint LGR
- 310 Pints/day capacity
- Built-in condensate pump
- Covers up to 5,000 sq ft


Moiswell Explorer V320
- 305 Pints/day capacity
- 412 CFM airflow
- Auto defrost and timer
7 Models Side by Side: Features, Best Use Cases, and Tradeoffs
The recommendations above are our strongest matches for different priorities. Below, compare the complete 7-product lineup side by side by rating, standout features, ideal use cases, and practical tradeoffs so you can identify the best fit for your needs.
- 310 Pints/day capacity
- Built-in condensate pump
- Covers up to 5,000 sq ft
- 180 Pints/day capacity
- Built-in pump
- Compact design
- 305 Pints/day capacity
- 412 CFM airflow
- Auto defrost and timer
- Built-in pump for drainage
- Covers up to 9,000 sq ft
- Auto defrost and restart
- 155 Pints/day capacity
- Built-in pump & drain hose
- Covers up to 7,500 sq ft

- 165 Pint capacity
- Built-in pump
- Faster defrost system

- 225 Pints/day capacity
- Automatic water pump
- 410 CFM airflow
7 Models Reviewed in Depth
#1. MOUNTO 310 Pint LGR
Max Capacity
Continuous Drain
Coverage Area
You’ll be impressed by the sheer dehumidifying power of the MOUNTO 310 Pint LGR, capable of extracting an incredible 310 pints per day while covering up to 5,000 sq ft. This makes it an exceptional choice for large-scale water damage restoration and demanding construction sites. The integrated condensate pump with a 15-foot lift ensures continuous, hassle-free drainage, and the advanced digital controls provide real-time humidity and temperature readings for precise job site management.
While its performance is outstanding, the 550 CFM airflow, though powerful, can contribute to a higher noise level. This unit is best suited for professionals tackling significant water issues or large commercial spaces where maximum moisture removal is the top priority. If you need a compact, quiet unit for a smaller area, this might be overkill, but for serious restoration work, it’s a top contender.
Pros
- Massive 310 PPD capacity
- Powerful 550 CFM airflow
- Built-in pump for continuous drainage
Cons
- Can be noisy
- Higher power consumption
- Heavy unit
Specifications
#2. ALORAIR Storm LGR Extreme
Restoration Capacity
Auto Drainage
Warranty
You’ll find the ALORAIR Storm LGR Extreme to be a top-tier choice for water damage restoration and demanding job sites, offering a substantial 180 pints/day capacity and a powerful 210 CFM airflow. Its compact design makes it surprisingly maneuverable for its power, fitting into tight spaces like crawl spaces and basements. The built-in pump simplifies drainage, and features like auto-restart and auto-defrost ensure continuous, hassle-free operation. This unit is also a good option for crawl spaces where humidity control is essential.
While its coverage area is listed at 2,300 sq ft, which is effective for many scenarios, you might need multiple units for extremely large or severely water-damaged areas. However, with its ETL safety compliance and an impressive 6-year warranty, this dehumidifier provides exceptional peace of mind and performance for professionals in the restoration industry.
Pros
- Excellent for water damage restoration
- Impressive 6-year warranty
- Compact and maneuverable design
Cons
- Coverage area may be limited for very large spaces
- Can be loud during operation
- Higher price point
Specifications
#3. Moiswell Explorer V320
Max Capacity
Airflow Rate
R32 Refrigerant
You’ll appreciate the exceptional dehumidification power of the Moiswell Explorer V320, boasting a massive 305 pints/day capacity and an impressive 412 CFM airflow, making it ideal for tackling severe humidity in large industrial spaces up to 9,000 sq ft. Its R32 system offers eco-friendly efficiency, while features like auto defrost, timer, and auto-restart after power outages ensure seamless operation.
While its robust performance is undeniable, be aware that this unit requires a 20 Amp receptacle due to its power needs. This is a serious workhorse for construction sites and industrial environments where consistent, high-level dehumidification is critical, but might be overkill for smaller, less demanding applications.
Pros
- Highest dehumidification capacity
- Powerful 412 CFM airflow
- Eco-friendly R32 system
Cons
- Requires 20 Amp receptacle
- Heavy-duty construction
- Not ideal for small spaces
Specifications
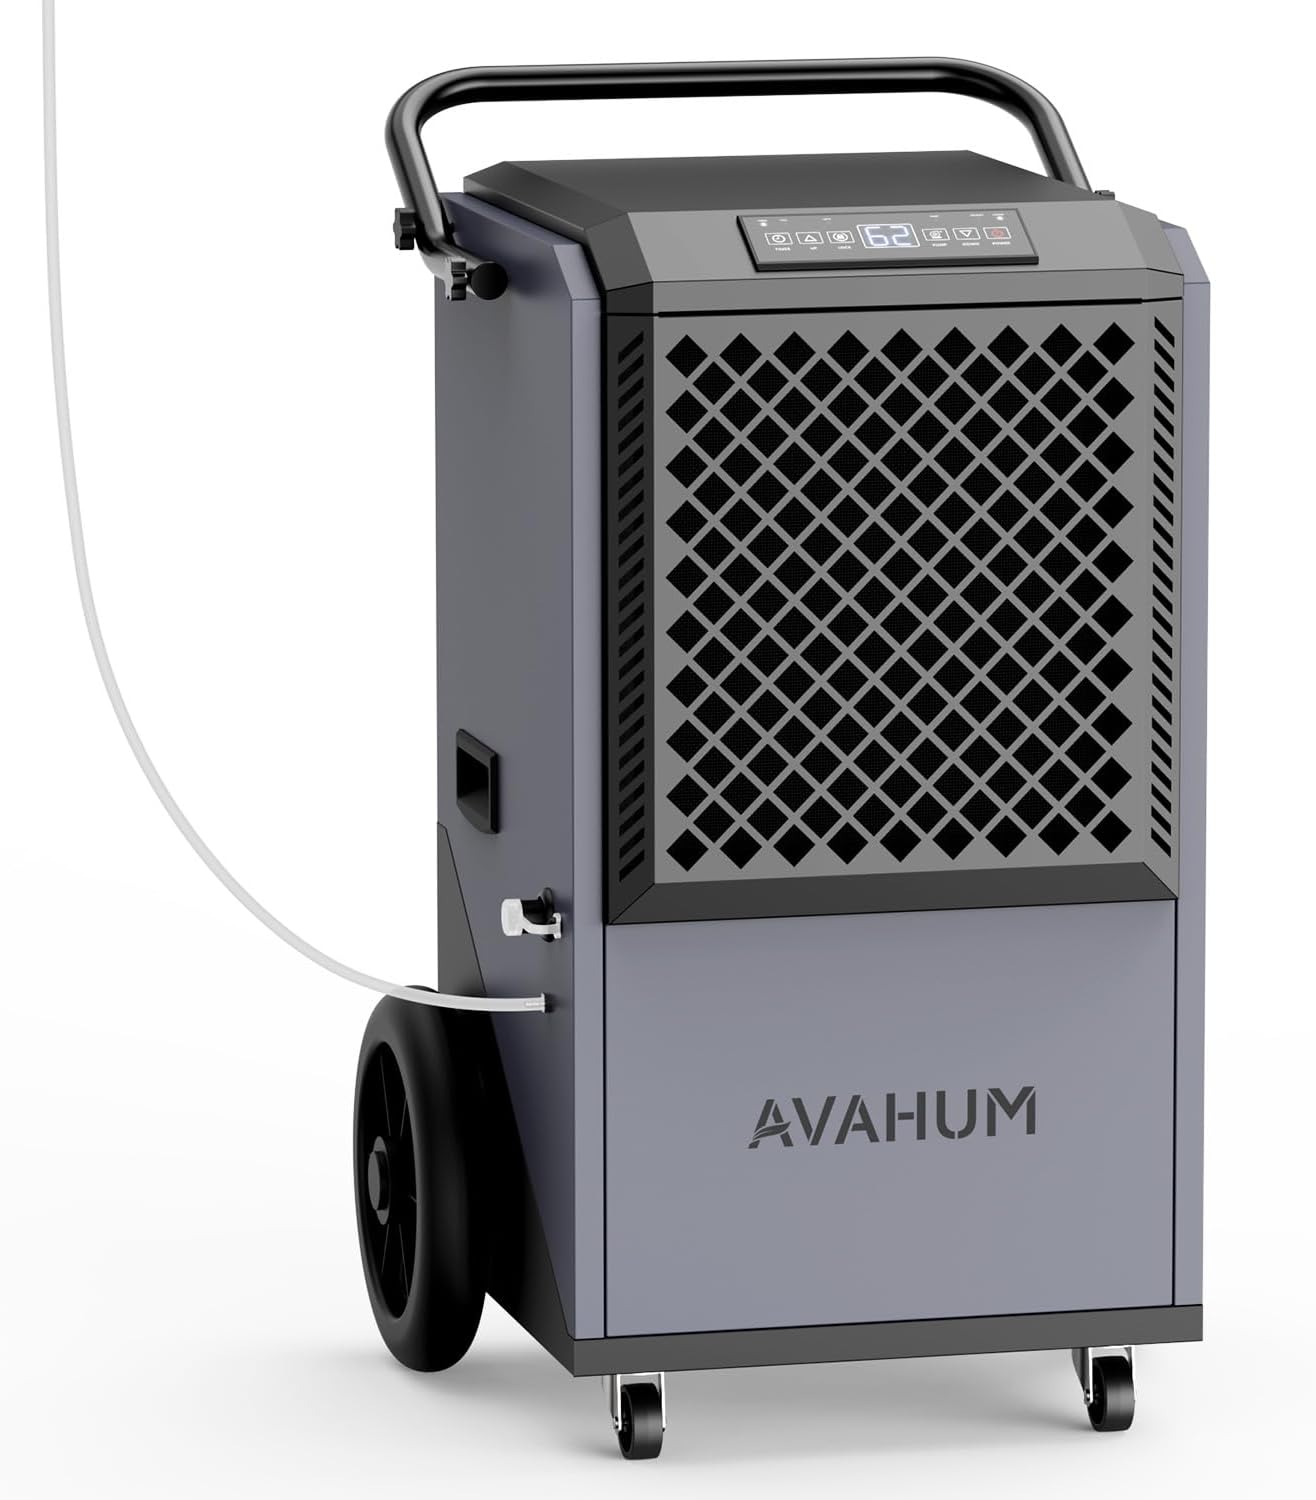
#4. AVAHUM Commercial 320 Pint
Daily Capacity
Continuous Drain
Max Coverage
You’ll find the AVAHUM Commercial Dehumidifier exceptionally capable for large spaces, with its 320-pint capacity and coverage for up to 9,000 sq ft, making it perfect for warehouses and construction sites. The integrated pump and included drain hose offer flexible, continuous drainage up to 16.4 ft, significantly reducing manual intervention. Its auto defrost, timer, and restart functions add to the convenience for long-term operation.
While it offers robust performance, the 8 reviews suggest it’s a newer model on the market. It’s a solid choice if you need reliable, high-capacity dehumidification for demanding commercial environments, but consider the limited review history if long-term durability is your primary concern.
Pros
- High 320-pint capacity
- Built-in pump with 16.4 ft lift
- Covers up to 9,000 sq ft
Cons
- Limited number of reviews
- Can be noisy
- Heavy unit
Specifications
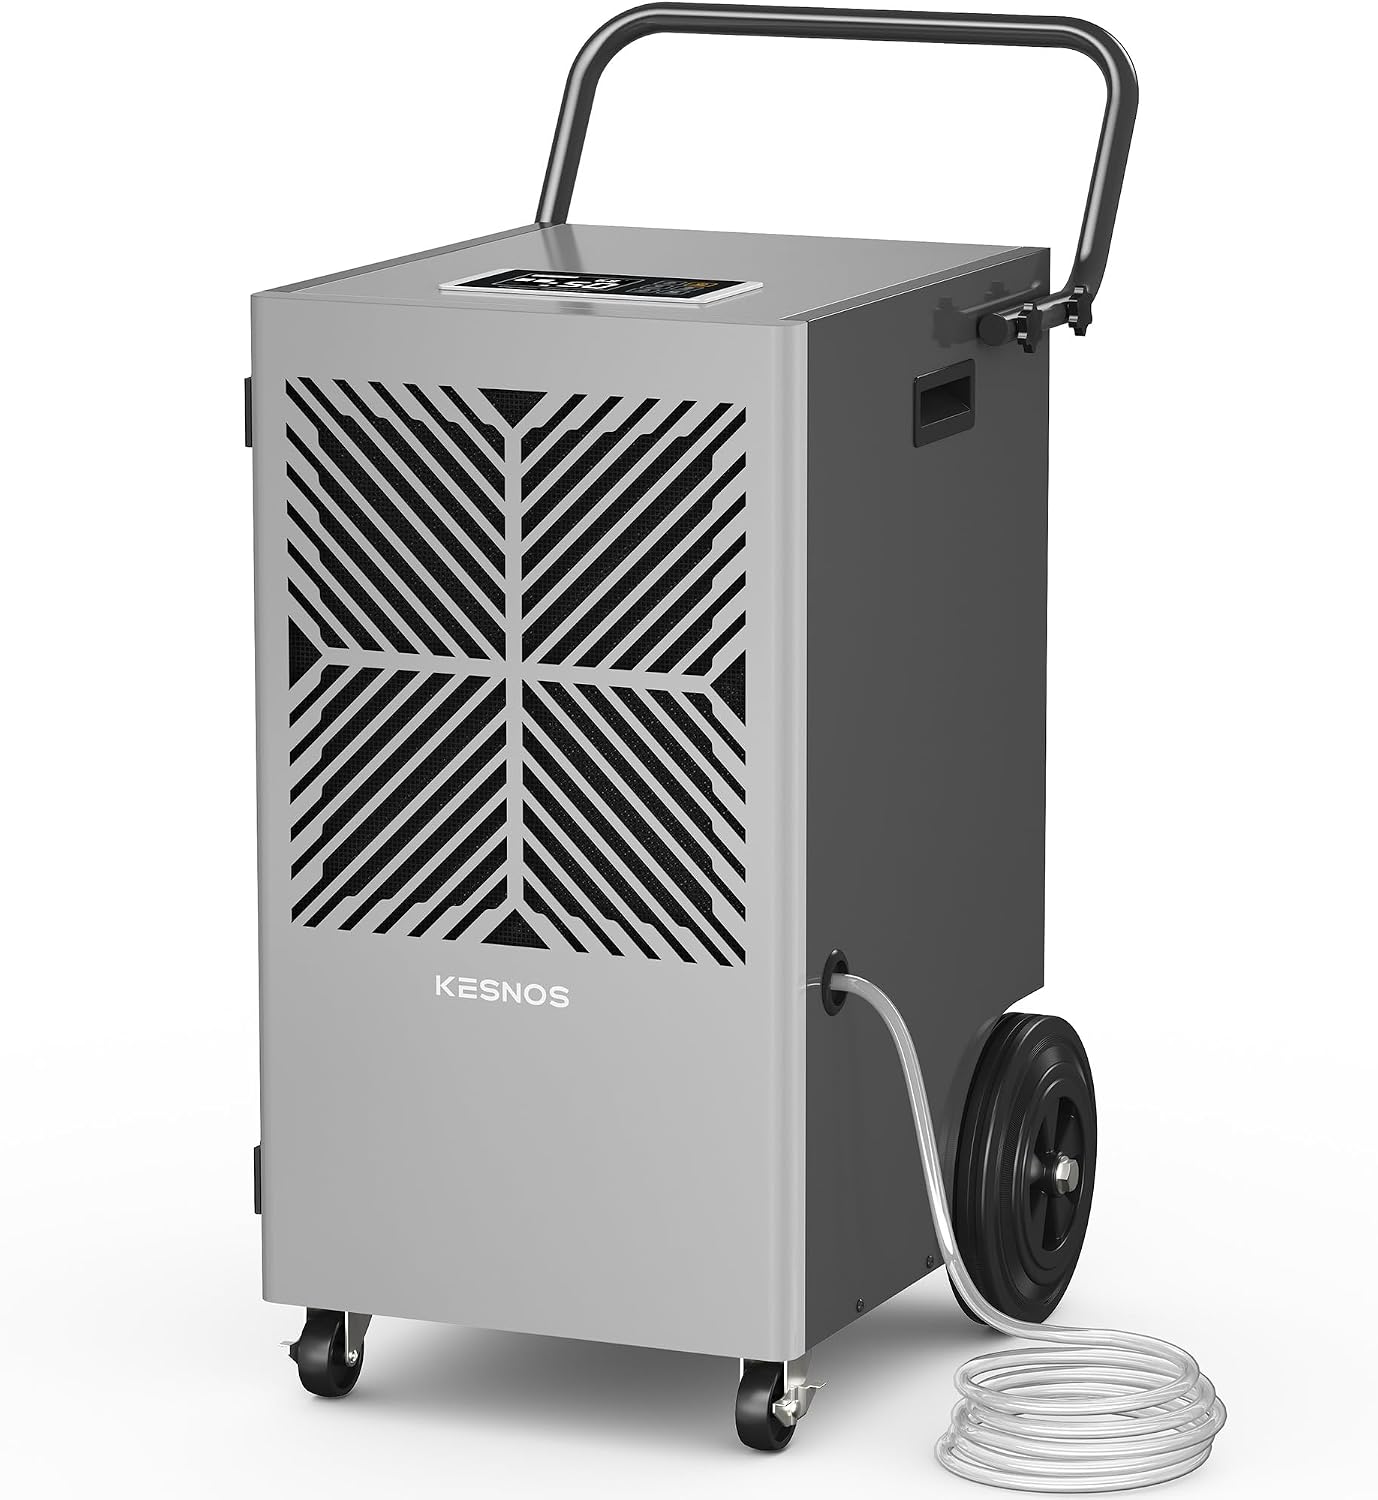
#5. Kesnos 155 Pint Commercial
Daily Capacity
Flexible Drainage
Coverage Area
You’ll find the Kesnos 155 Pint Commercial Dehumidifier a reliable workhorse for demanding job sites and large spaces up to 7,500 sq ft. Its 155 pints/day capacity and 164.7 CFM airflow ensure efficient moisture removal, while the built-in pump and dual drainage options offer great flexibility. The portable design with large wheels and a foldable handle makes it easy to maneuver around various work environments.
While it offers excellent features for its class, some users might find the 155-pint capacity slightly less than the top-tier models for extremely water-logged areas. It’s an excellent choice for general construction site use, basements, and workshops where portability and effective dehumidification are key, but if you’re dealing with severe, widespread water damage, you might consider a higher-capacity unit.
Pros
- Excellent portability for job sites
- Built-in pump with flexible drainage
- Good coverage for large areas
Cons
- Capacity may be insufficient for extreme water damage
- Can be loud
- Filter requires regular cleaning
Specifications
#6. TURBRO 165 Pint Commercial
Defrost System
Continuous Drain
Eco-Friendly
You’ll appreciate the TURBRO 165 Pint Commercial Dehumidifier’s efficient operation, especially in cold and humid conditions, thanks to its faster defrost system that reduces downtime by 50%. It effectively dehumidifies areas up to 7,500 sq ft, removing up to 165 pints per day. The built-in pump and included hose offer convenient continuous drainage, and its large wheels and handles make it easy to move around job sites.
While the faster defrost is a significant advantage, some users might find the 276 CFM airflow less powerful than higher-end models for extremely rapid drying needs. This unit is a great choice for construction sites, warehouses, and basements, particularly in environments where lower temperatures are common, offering a good balance of performance and efficiency.
Pros
- Faster defrost system
- Built-in pump for continuous drainage
- Good for cold, humid conditions
Cons
- Lower airflow than some competitors
- Limited number of reviews
- Can be bulky
Specifications
#7. BlueDri BD-130P
Max Capacity
Easy Drain
Airflow
You’ll appreciate the high capacity of the BlueDri BD-130P, capable of removing up to 225 pints per day, making it a strong contender for basement restoration and job sites. Its automatic water pump and 410 CFM airflow ensure efficient moisture removal and drainage, while features like auto-restart and a digital panel simplify operation. The heavy-duty roto-mold construction suggests durability for demanding environments.
However, with a 3.6-star rating from 168 reviews, some users have reported issues with reliability or longevity. While it offers significant power for its price point, consider this a solid option if budget is a primary concern for tasks like basement drying or moderate water damage restoration, but be prepared for potential maintenance needs.
Pros
- High 225-pint capacity
- Automatic pump and drainage
- Powerful 410 CFM airflow
Cons
- Lower average customer rating
- Potential reliability concerns
- Heavy unit
Specifications
Taming the Damp: Your Guide to Construction Site Dehumidifiers
Keeping a construction site dry is crucial for project timelines, material integrity, and worker safety. Excess moisture can lead to mold growth, damage sensitive materials like drywall and lumber, and even compromise structural elements. Investing in the right industrial dehumidifier isn’t just about convenience; it’s about protecting your investment and ensuring a quality finished product.
The Pillars of Performance: What to Prioritize
When selecting an industrial dehumidifier for a demanding construction environment, several key attributes deserve your attention.
- Moisture Removal Capacity: This is the primary function. Look for units designed to handle significant amounts of water extraction in large, often unconditioned spaces.
- Durability and Ruggedness: Construction sites are tough environments. Your dehumidifier should be built to withstand dust, debris, and the general wear and tear of daily operation.
- Portability and Placement: Consider how easily the unit can be moved around the site and where it will be positioned. Features like sturdy wheels and a manageable size can make a big difference.
- Drainage Options: Think about how the collected water will be managed. Continuous drainage hoses are often essential for uninterrupted operation, preventing frequent emptying.
- Operating Temperature Range: Ensure the dehumidifier is designed to function effectively in the typical temperature fluctuations you’ll encounter on your site, from cooler mornings to warmer afternoons.
Common Traps That Can Sink Your Purchase
Navigating the options can be tricky. Be aware of these common missteps.
- Underestimating the required capacity for your specific site size and moisture levels.
- Overlooking the importance of a robust, job-site-ready build that can handle dust and impact.
- Failing to plan for water drainage, which can lead to constant interruptions and reduced efficiency.
Seal the Deal: Your Top Construction Site Dehumidifier Picks
For heavy-duty water removal and rapid drying, the MOUNTO 310 Pint LGR is your powerhouse. If a long warranty is your priority, the ALORAIR 180 PPD stands out. For versatile coverage up to 9,000 sq. ft. with smart features, the 320 Pint Commercial Dehumidifier is a solid contender. The Kesnos 155 Pints and TURBRO 165 Pint offer excellent performance for large spaces, while the BlueDri BD-130-BL is a reliable workhorse for various job sites.
All these industrial dehumidifiers are designed to tackle moisture head-on, ensuring your construction projects stay on track. Don’t let dampness slow you down – check current availability to secure the best unit for your needs today!
Final 3 Picks: Large restoration jobs, Water damage restoration, and Heavy-duty industrial use
Ready to decide? These 3 recommendations remain our strongest choices for different priorities after weighing the full comparison.
MOUNTO 310 Pint LGR
- 310 Pints/day capacity
- Built-in condensate pump
- Covers up to 5,000 sq ft
Moiswell Explorer V320
- 305 Pints/day capacity
- 412 CFM airflow
- Auto defrost and timer
